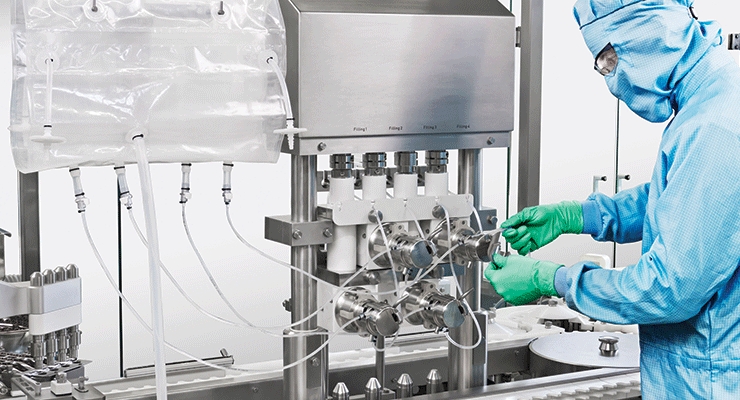
Experience world-class dietary supplement manufacturing with our state-of-the-art facilities, cutting-edge automation, and unparalleled production capacity. From small batches to large-scale operations, we deliver excellence at every level.
Our world-class manufacturing capabilities combine advanced automation, precise quality control, and scalable production systems to deliver consistent, high-quality dietary supplements for global markets.
Advanced rotary tablet presses with real-time weight control
95% capacity utilization
High-speed encapsulation with automated quality inspection
88% capacity utilization
Rotary die encapsulation with gelatin and vegetarian options
82% capacity utilization
Our manufacturing floor houses the industry's most advanced equipment, featuring automated production lines, precision dosing systems, and integrated quality control mechanisms that ensure consistent product quality and maximum efficiency.
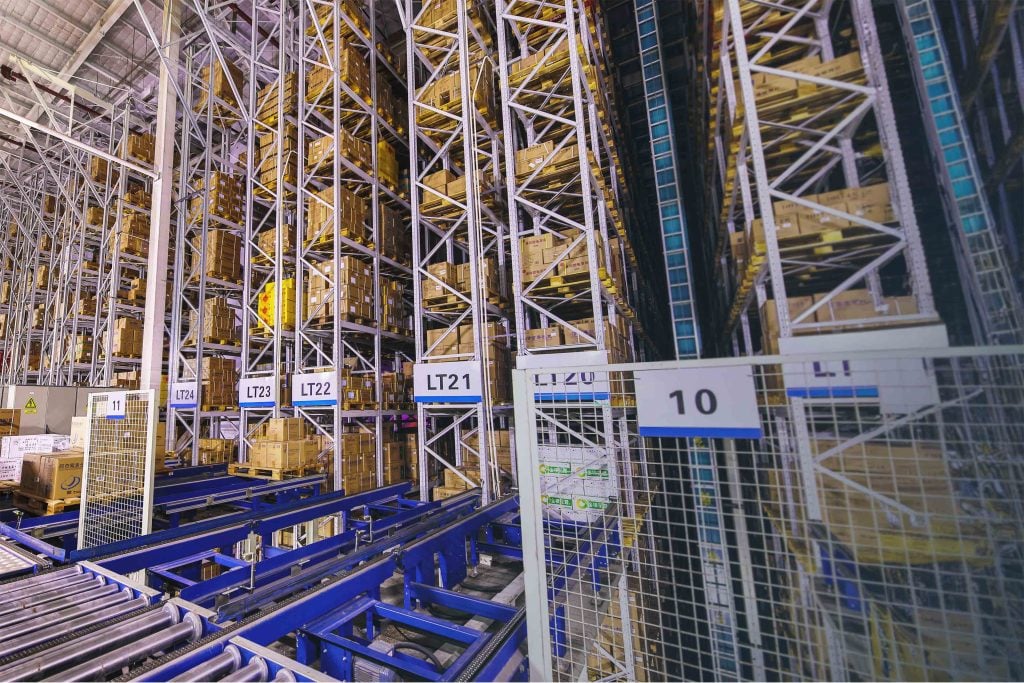
Our fully automated warehousing and material handling systems ensure optimal inventory management, reduced human error, and maximum operational efficiency. Advanced robotics and AI-driven logistics optimize every aspect of our supply chain.
Our facilities maintain the highest regulatory standards with comprehensive certifications that ensure global market access. Our quality management systems exceed industry requirements and provide complete traceability throughout the manufacturing process.
Our ISO 17025 accredited laboratory is equipped with cutting-edge analytical instrumentation and staffed by PhD-level scientists. We provide comprehensive testing services that exceed industry standards and ensure product safety, efficacy, and compliance.
From startup quantities to large-scale commercial production, our flexible manufacturing systems adapt to your business needs. Our modular production approach ensures seamless scaling without compromising quality or efficiency.
Product development and market testing
Full market launch and distribution
High-volume production for established brands
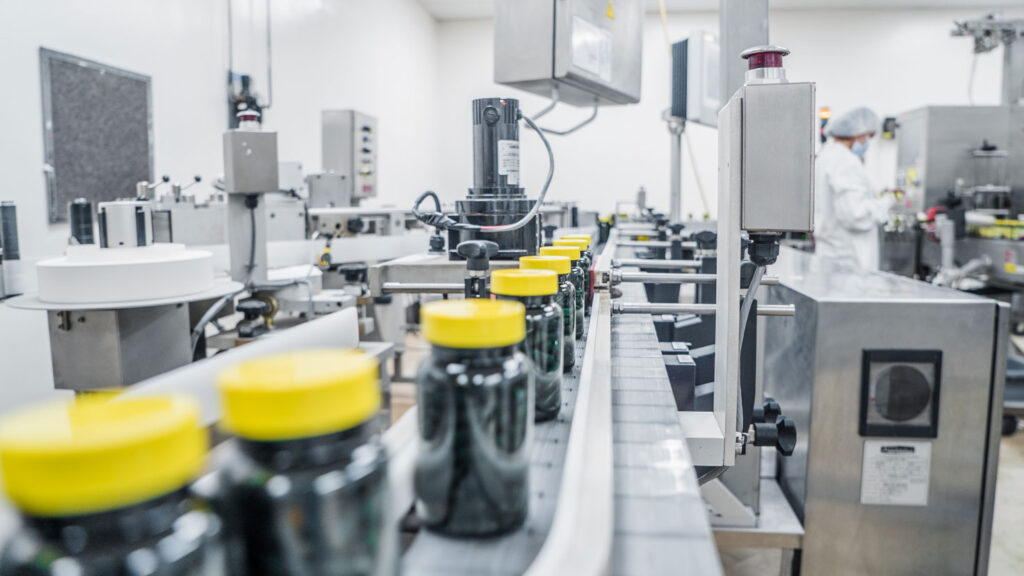
Our 150,000 square foot manufacturing complex represents the pinnacle of modern supplement production technology.